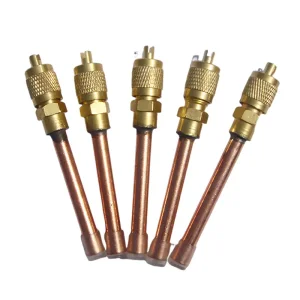
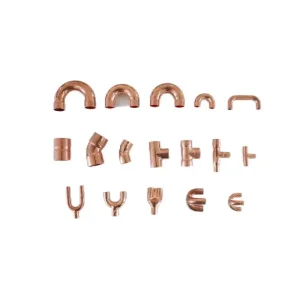
High-performance components engineered for severe climatic operations, ensuring maximal thermal exchange efficiency.
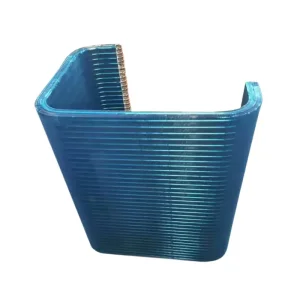
A strategic analysis of thermal management requirements in North Africa's booming commercial sectors.
As Benghazi rapidly modernizes its commercial, maritime, and cold-chain infrastructure, the demand for exceptionally resilient thermal management equipment has reached unprecedented levels. Operating in North Africa’s Mediterranean coastal climate demands specialized hardware capable of withstanding high ambient temperatures, elevated relative humidity, and airborne saline particulate matter. Standard off-the-shelf heat exchangers frequently suffer from accelerated galvanic corrosion and thermal efficiency degradation. Consequently, industrial buyers, commercial cold storage operators, and HVAC contractors across Benghazi increasingly mandate high-grade finned condensers engineered for maximum thermal dissipation and structural longevity.
Ningbo Taojun Refrigeration Equipment Co., Ltd. (founded in 1988, originating from the Xiangshan Refrigeration Accessories Factory of Zhejiang University) leverages over three decades of engineering expertise to supply world-class components. Our finned condensers incorporate precision-extruded copper tubing integrated mechanically or hydraulically with high-purity aluminum or copper fins, ensuring optimal contact conductance and rapid thermal transfer. Utilizing state-of-the-art German manufacturing equipment, automated CNC tube benders, and rigorous helium leak-detection systems, we eliminate micro-fractures and structural weaknesses.
Bridging academic research from Zhejiang University with high-volume industrial production.
Our R&D center houses 15 senior engineers holding advanced degrees from top-tier research institutions, continuously innovating refrigerant flow dynamics and corrosion-resistant coatings.
Employing a strict 5D quality assurance framework, every production batch undergoes extensive thermal shock testing, salt-spray resistance evaluation, and 100V high-voltage breakdown checks.
Trusted strategic supplier to global appliance leaders including Haier, Midea, Gree, and Whirlpool, delivering bespoke thermal systems tailored to regional environmental specs.
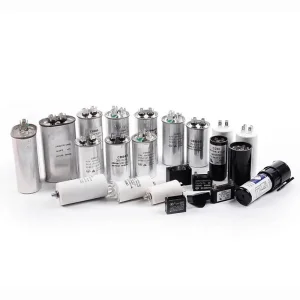
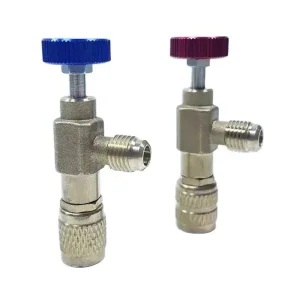
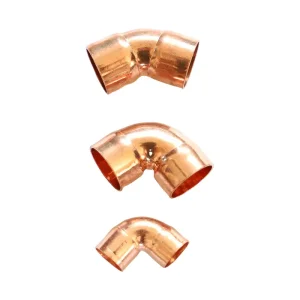
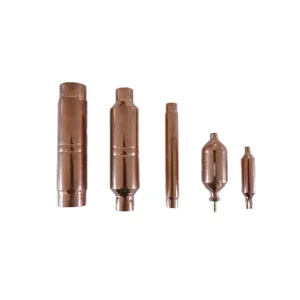
Explore our comprehensive inventory of certified components designed for seamless system integration.
Expert answers regarding technical specifications, shipping to Benghazi, and custom OEM manufacturing.
Our finned condensers undergo rigorous protective treatments including high-grade anti-corrosion hydrophilic or epoxy-coated aluminum fins and robust copper tubing. This design effectively resists salt-spray degradation and extreme thermal fluctuations common in North African coastal environments.
Yes. With 15 senior engineers and fully automated production lines, we support custom sizing, tube configurations, circuit arrangements, and pressure ratings tailored precisely to your equipment requirements.
Standard manufacturing orders are completed within 15 to 25 days, backed by our efficient global logistics network ensuring prompt, secure maritime or air freight delivery directly to Benghazi port facilities.
Our facilities are fully certified under GB/T19001-2016/ISO9001:2015 quality management standards, EU RoHS environmental directives, and US UL certifications, guaranteeing uncompromised reliability.
 Taojun