High-purity brass, copper fittings, and molecular sieve driers optimized for system purity and heat exchange efficiency.
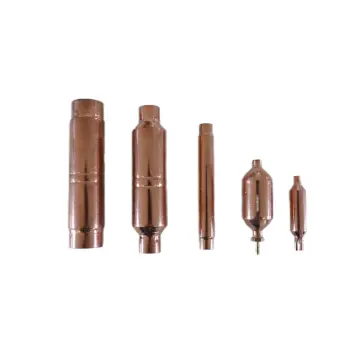
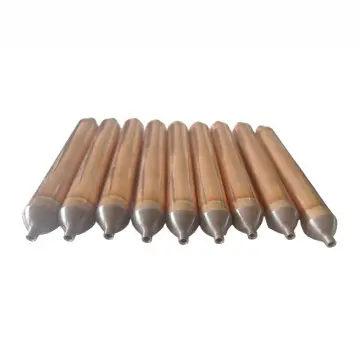
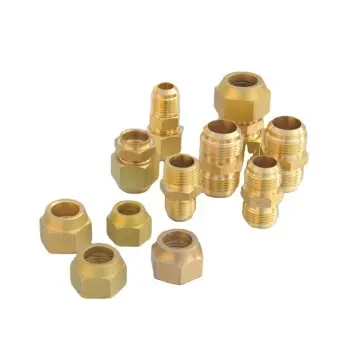
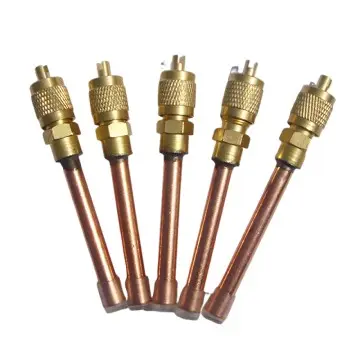
Founded in 1988 as the Xiangshan Refrigeration Accessories Factory of Zhejiang University, Ningbo Taojun Refrigeration Equipment Co., Ltd. has developed over three decades into a leading force in high-precision refrigeration manufacturing. Our facility in Xiangshan, Ningbo blends academic-driven research with high-volume industrial capability.
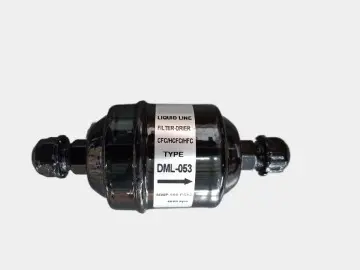
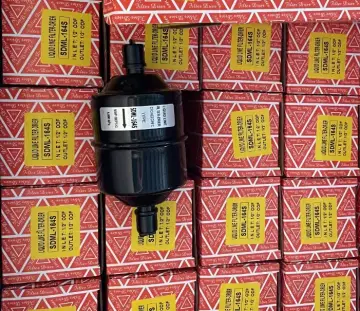
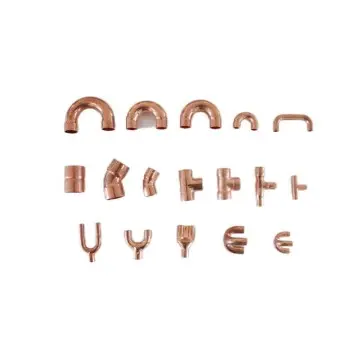
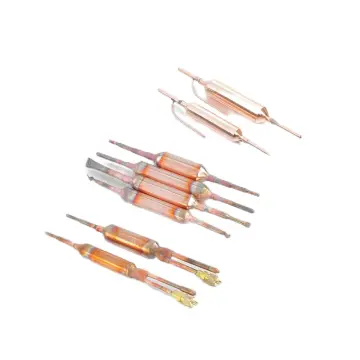
We are a certified national high-tech enterprise. Our core product portfolio includes molecular sieve filter driers, check valves, air conditioning valves, condensers, brass and copper accessories, and thermal insulation wrap systems. Guided by our "Lingshan" brand, we build for high-pressure, zero-leak commercial and residential HVAC/R setups.
Our infrastructure holds ISO 9001:2015, EU RoHS, and US UL safety listings. We serve top-tier global manufacturers, supplying stable OEM and ODM component paths to brands like Haier, Midea, Gree, Whirlpool, Electrolux, and Huarui.
How our copper filter driers keep high-pressure refrigerants clean, dry, and acidic-free.
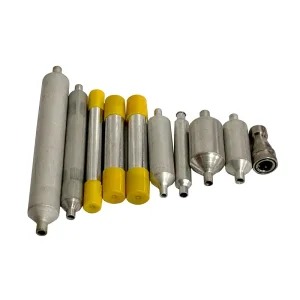
We use premium 3A molecular sieves. This synthetic zeolite features controlled 3-angstrom pores that selectively capture water molecules (pore diameter ~2.8Å) while leaving refrigerant molecules untouched (R134a, R32, R410A, and R290 all exceed 3.9Å). This prevents system performance drops from co-adsorption.
Our driers feature a dual-stage core. First, high-purity zeolite beads adsorb moisture down to 10 ppm. Next, a blended activated carbon layer neutralizes organic acids, varnish, and sludge. This prevents acid-induced compressor motor burnout.
We use automated argon arc welding on high-purity deoxidized copper tubing (DHP grade, Cu ≥ 99.9%). This keeps structural joints strong and prevents leaks at high operating pressures (over 60 bar / 870 PSI), matching the demands of modern R410A and R32 high-pressure systems.
How we design next-generation filtration to support low-GWP refrigerants and green cooling tech.
Transitioning to natural refrigerants like R290 (propane) and R744 (CO₂) requires high safety margins. Our newest series handles high operating pressures and low-viscosity flow profiles safely.
We are prototyping sensor-enabled driers. These units track pressure drops (ΔP) and moisture levels in real-time, letting operators service systems before a breakdown occurs.
Micro-channel heat exchangers plug easily. We have added ultra-fine mechanical mesh filters (down to 10 microns) to trap debris before it enters the condenser pathways.
To support global environmental initiatives, we are shifting all brass fittings and connector valves to lead-free formulations, keeping compliance ahead of RoHS regulations.
How our advanced manufacturing systems ensure zero-defect product runs.
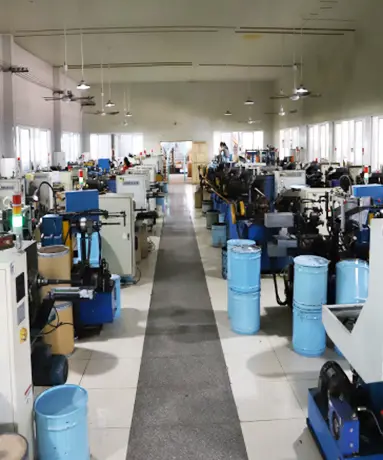
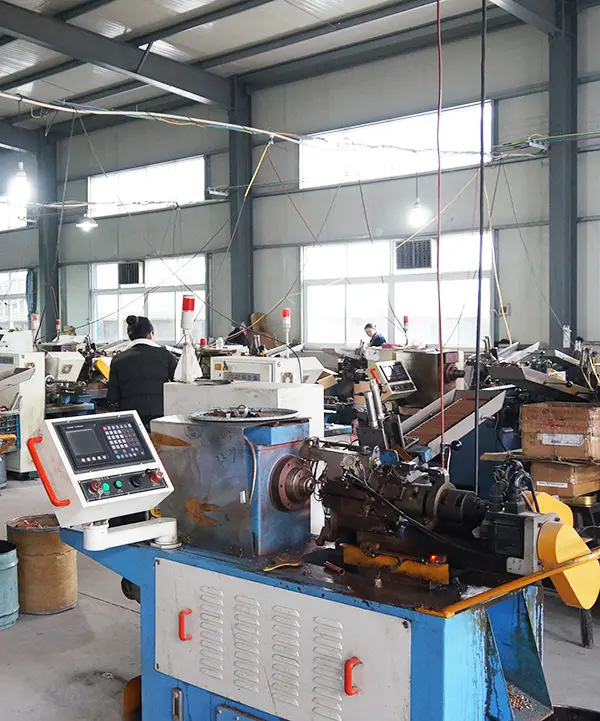
We use high-precision automated manufacturing equipment imported from Germany to guarantee consistent wall thickness and fitting tolerances.
Our design center features 15 lead engineers, with key specialists holding advanced degrees from the University of Science and Technology of China (USTC).
We source ITO materials and liquid crystal spacers from Japan. Protective films withstand extreme temperatures (80-90°C) without shrinking or changing color.
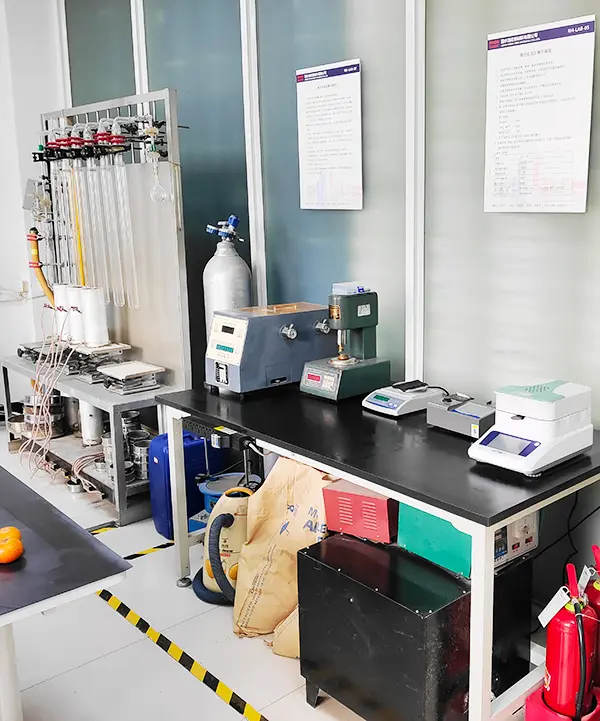
Finished driers undergo 500-hour environmental chamber runs at -35°C to 75°C and thermal shock testing to verify mechanical strength.
Every dry filter and valve is pressure-tested. Smart sheets undergo 24-hour aging checks, and roll films face 100V high-voltage insulation tests.
Our Ningbo production center uses advanced manufacturing technology to optimize cost and quality. Our MES (Manufacturing Execution System) tracks parts in real time, from raw copper receipt through molecular sieve filling to final welding.
Located near the deep-water Port of Ningbo, we ship to major global ports with short transit times. Our automated raw material handling and scale keep production steady, shielding buyers from sudden price changes and material shortages.

Tailoring our HVAC driers and accessories for specific B2B industrial needs.
Truck and train refrigeration systems face constant vibrations. We build reinforced internal spring packs and shock-resistant molecular sieve beds to keep the desiccant core from fracturing during transport.
Modern heat pumps reverse flow direction between heating and cooling cycles. We supply dual-flow copper filter driers that filter out contaminants and moisture in both directions, eliminating the need for two separate check-valve installations.
Medical freezers run at very low temperatures (down to -80°C), where even minor moisture freezes expansion valves. We use specialized, high-density zeolite compounds to capture trace water at low temperatures.
We provide localized engineering support and customer service teams to help global buyers manage design, regulatory compliance, and shipping processes. From customs clearance help to on-site engineering consultations, we support your logistics team directly.
Our quality system is verified under GB/T19001-2016/ISO9001:2015 (Registration No.: 41325Q00065R0S). Our parts are fully compliant with RoHS and REACH requirements, making them ready for immediate integration in European and American production plants.
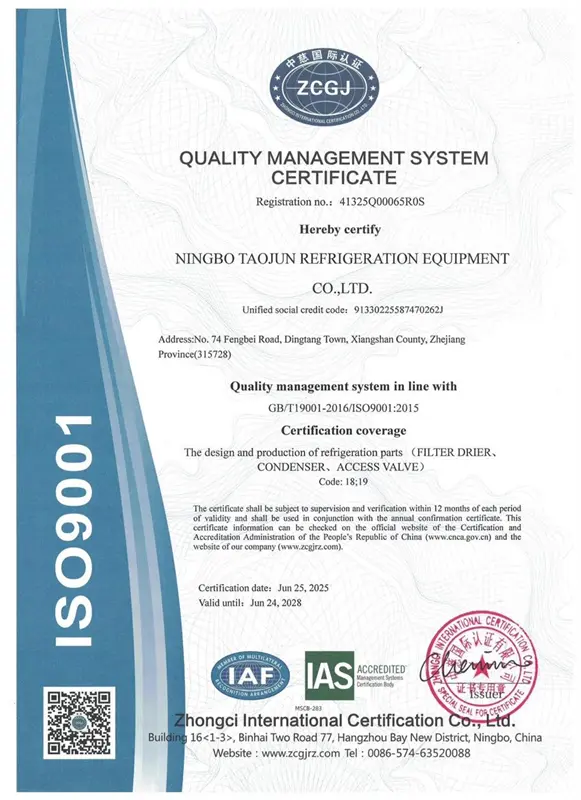
Main Certification Document
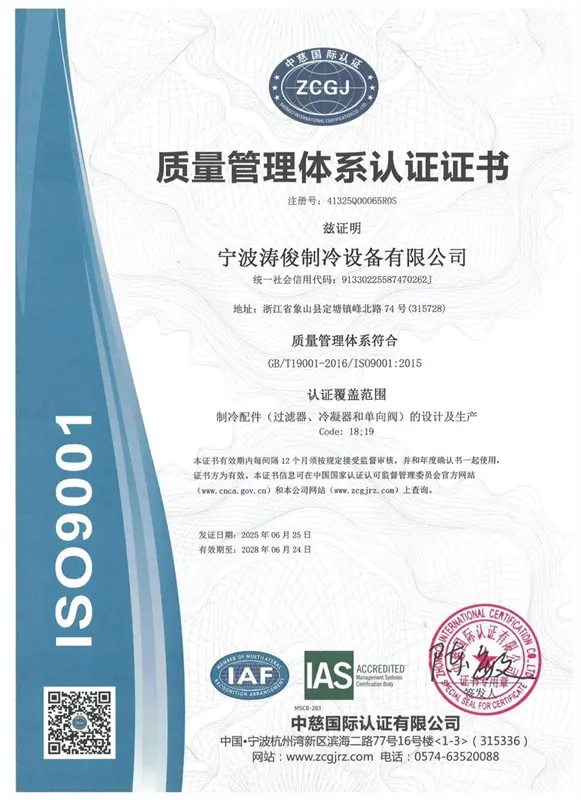
Detailed Scope of Certification
Technical answers to key questions from B2B buyers and refrigeration engineers.
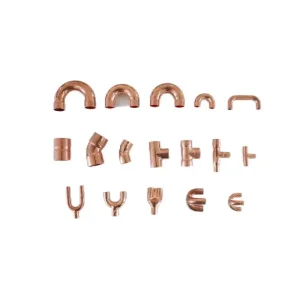
Industrial-grade line components, heavy-duty charging lines, and specialized copper fittings for global distributors.
 Taojun